
 EN
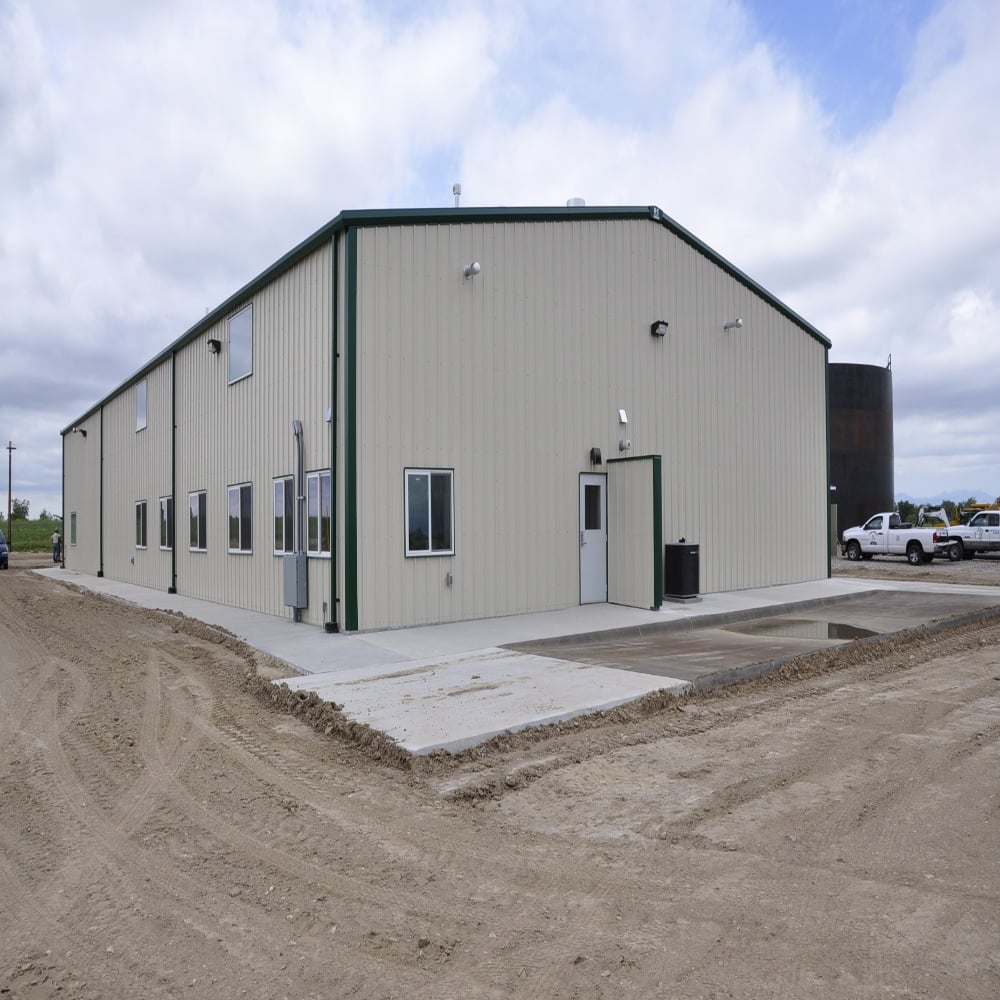
Structural Design Principles for Heavy-Duty Steel Construction
Load Path Analysis for Crane Systems and Process Equipment
A clearly defined load path is the foundation of heavy-duty steel construction—ensuring forces from overhead cranes and vibrating process equipment travel efficiently to the foundation without overloading individual members. The analysis begins by quantifying vertical wheel reactions, lateral thrust from crane acceleration, and longitudinal braking forces. Per CMAA 74, a typical 20-ton overhead crane imposes wheel loads exceeding 200 kN per end truck, with lateral forces reaching up to 20% of the lifted load. These forces transmit through runway beams, support brackets, columns, and bracing—requiring deliberate sequencing of connections to eliminate hidden stress concentrations. For dynamic equipment like crushers or mixers, amplification factors of 1.25–1.50 account for impact and vibration effects. Finite-element modeling helps visualize stress flow and pinpoint locations needing local stiffening or supplemental bracing. Without continuity and coherence in the load path, even oversized members risk fatigue cracking at connection interfaces. Engineers therefore treat the entire steel assembly as an integrated force-conveyance system—not merely discrete components.
AISC 360 & AISC N690 Compliance in High-Moment Connections
High-moment connections in industrial steel structures must comply with AISC 360 for general building design—and, where safety-critical performance is required, the enhanced provisions of AISC N690. AISC 360 mandates that moment connections sustain at least 1.1 times the plastic flexural strength of the connected beam, promoting ductile behavior under overload and mitigating brittle fracture in cyclic crane-loading environments. For facilities handling hazardous materials or supporting mission-critical production, AISC N690 introduces additional safeguards: higher weld-toughness requirements (e.g., Charpy V-notch toughness of 40 J at –29°C versus 27 J at –18°C for standard AISC 360), mandatory post-weld heat treatment, and connection details designed to remain elastic beyond design-basis events. By aligning with both standards, engineers ensure connections withstand not only peak moments but also decades of cumulative fatigue and thermal cycling—preserving structural integrity across the facility’s service life.
Crane Integration and Runway System Engineering in Steel Construction
Dynamic Load Amplification per CMAA 74 and Runway Beam Deflection Control
Crane runway beams must resist amplified dynamic forces—not just static weight. CMAA 74 specifies vertical load factors of 1.25 for hoist loads and 1.10 for trolley dead loads to account for inertia, impact, and sudden load shifts during operation. These multipliers convert nominal crane capacity into realistic design loads. Vertical deflection is tightly controlled: CMAA 74 recommends limits of L/600 for standard cranes and L/1000 or better for precision applications—where rail misalignment could accelerate flange wear or induce wheel binding. In integrated steel framing, runway beams often serve dual roles—supporting both roof loads and crane reactions—eliminating separate support columns and maximizing clear floor space. To meet deflection criteria, engineers may increase beam depth, optimize moment of inertia, or specify higher-strength steels. Lateral sway is managed via horizontal bracing and stiffened connections, while combined vertical/horizontal deflection is assessed to preserve rail alignment and prevent premature fatigue. Adherence to CMAA 74’s dynamic and deflection guidelines ensures long-term reliability, minimal maintenance, and safe interaction between crane and structure.
Optimizing Clear-Span Layouts and Column-Free Interiors
Truss, Vierendeel, and Mega-Frame Solutions for 45+ Meter Spans
Column-free interiors spanning 45 meters or more require purpose-built primary framing systems—each balancing structural efficiency, functional clearance, and architectural intent. Three proven approaches dominate heavy steel construction: trusses, Vierendeel girders, and mega-frames.
Trusses (spans 45–80 m) resolve bending into axial forces through triangulated webs, achieving depth-to-span ratios of 1/12–1/15. They are well-suited for standard crane workshops, with deflection governed by AISC 2022 limits of L/600 under full live load. Where web diagonals interfere with crane runways, Vierendeel frames—using rigid joints and member stiffness instead of diagonal bracing—span 40–60 m while maintaining unobstructed passage.
For spans beyond 60 m or high-dynamic-load environments, mega-frames with deep built-up or cellular beams deliver superior performance. A 2021 study found optimized mega-frames with moment-resisting knees reduced steel tonnage by 15% compared to equivalent truss schemes—while fully accommodating 50-ton crane reactions. Integrating these systems allows flexible, future-ready layouts that preserve structural integrity and operational adaptability.
Floor Systems and Material Strategy for Long-Term Steel Construction Performance
Floor systems and material selection directly shape long-term durability in demanding industrial settings. The following strategies target sustained performance under heavy traffic, corrosion exposure, and seismic demand.
Jointless Post-Tensioned Slabs for Heavy Forklift Traffic
Jointless post-tensioned slabs eliminate contraction joints—vulnerable points for cracking and edge spalling under repeated heavy forklift loading. By introducing compressive stress into the concrete, post-tensioning increases tensile capacity, enabling thinner slabs without compromising load rating. This approach reduces concrete volume by up to 25% versus conventional jointed designs (ACI 2022). The seamless surface minimizes tire wear and simplifies cleaning and maintenance. Critical to success is precise tendon layout and stressing sequence to ensure uniform compression and avoid curling-induced differential settlement. Specialized detailing at column penetrations and steel-frame interfaces guarantees robust load transfer—enhancing overall system resilience. In steel-framed industrial buildings, jointless slabs significantly extend service life and reduce lifecycle repair costs.
ASTM A992 vs. A572 Grade 50: Corrosion Resistance and Seismic Fabrication Readiness
Material selection balances environmental exposure, structural function, and constructability. ASTM A992—the standard specification for wide-flange shapes in building framing—offers superior seismic readiness due to its maximum yield-to-tensile ratio of 0.85, guaranteed 50-ksi minimum yield strength, and tightly controlled carbon equivalent. These properties improve weldability, reduce preheat requirements, and support reliable plastic hinge formation in moment frames designed per AISC 341. In contrast, ASTM A572 Grade 50 (particularly Type 1, copper-bearing) provides enhanced atmospheric corrosion resistance—forming a protective oxide layer suitable for uncoated secondary members in mildly corrosive environments. While not a substitute for coatings in aggressive chemical settings, it extends maintenance intervals where corrosion governs longevity. Fabricators prefer A992 for its consistent mechanical properties and compatibility with prequalified welding procedures; A572 may require additional procedure qualification for critical joints. Selection hinges on structural role: A992 for primary lateral-force-resisting elements in seismic zones; A572 for non-critical, corrosion-exposed members where long-term maintenance planning drives material choice.
FAQ
What are key considerations when designing load paths in heavy-duty steel construction?
Key considerations include analyzing vertical wheel reactions, lateral and longitudinal forces, dynamic forces from equipment, using finite-element modeling to visualize stress flow, and ensuring a seamless load path to prevent stress concentrations and fatigue.
How do AISC 360 and AISC N690 impact the design of high-moment connections?
Both standards ensure safety and durability. AISC 360 promotes ductile behavior under overload, while AISC N690 adds higher weld-toughness and heat treatment requirements to manage cumulative fatigue and thermal cycling in safety-critical structures.
What methods improve crane runway beam performance?
To optimize crane runway beams, engineers utilize CMAA 74 guidelines, control vertical deflection, increase beam depth, add horizontal bracing, and use high-strength materials to align both vertical and horizontal deflection for long-term durability.
What's the best approach for designing column-free interiors over large spans?
Effective approaches include trusses for spanning 45–80 meters, Vierendeel girders for unobstructed passage up to 60 meters, and mega-frames for spans beyond 60 meters and high-dynamic-load settings, emphasizing flexibility and load optimization.
How do jointless post-tensioned slabs impact industrial flooring?
Jointless post-tensioned slabs reduce cracking and edge spalling due to forklift traffic, minimize maintenance, and ensure durability by eliminating contraction joints while optimizing load-bearing performance through compressive stress.
When should ASTM A992 or ASTM A572 Grade 50 steel be used?
ASTM A992 is ideal for seismic-prone areas due to high ductility and weldability, while ASTM A572 Grade 50 is suitable for corrosion-exposed, non-critical elements in industrial settings requiring enhanced resistance and low maintenance.